

‹
›
‹
›
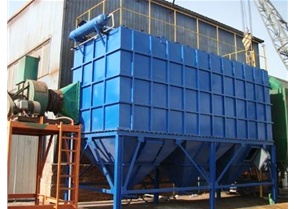
Boiler Dust Collector / Boiler Bag Filter
Product Details
Product Overview
The boiler dust collector is a modular, unit-combination dust collection device featuring large air handling capacity, low filtration velocity, good cleaning effectiveness, high dust collection efficiency, reliable operation, convenient maintenance, and a small footprint. With modular production, product quality is consistent and stable. It is widely used for boiler flue gas treatment, dust recovery, and dust control in industries such as power, metallurgy, building materials, and chemicals.
System Composition
The boiler dust collector consists of the following components:
XLDM Series Offline Cleaning Low-Pressure Pulse Baghouse Collector Body: Features stable operation, low resistance, low energy consumption, good cleaning effectiveness, and a small footprint.
Protection System
Compressed Air System: Includes air storage tank, oil-water separator, and piping.
Control System: Includes instruments, PLC cabinet, MCC cabinet, and field operation cabinet.
Working Principle
Flue gas enters the venturi through the inlet duct. At the throat inlet, water is evenly sprayed in. Due to the high-velocity movement of the flue gas, the sprayed water is atomized into fine water mist that wets the ash particles in the flue gas. As a result, the ash particles and water droplets collide and coalesce. Particularly fine dust particles can be dissolved by the water mist. This achieves primary dust removal and desulfurization, fully preparing the ash particles for separation.
The flue gas then enters the main body, where the rapidly cooled gas continues to impact the lime water in the tank. Dust and SO₂ in the flue gas react with the lime water to form sulfates. Under the combined action of inertial force, gravity, adhesion, and cohesion, these settle to the bottom, completing the secondary desulfurization process.
The water splashes and water mist generated by the flue gas, together with the washed flue gas, rise simultaneously under the suction of the fan, allowing the flue gas to fully react with the lime water. The gas-water mixture then passes through an impeller dehydrator for gas-water separation. Water flows through a drain pipe back into the water tank. The flue gas undergoes tertiary dust removal and desulfurization, after which the purified gas is discharged into the atmosphere by the fan.
Cleaning System
The boiler dust collector uses three-state offline pulse cleaning, automatically controlled by a PLC. As the dust collector operates, dust accumulates on the surface of the filter bags, gradually increasing gas flow resistance. When the resistance increases to a preset value, the PLC initiates a cleaning cycle for each compartment according to the selected control mode (differential pressure control, time control, or manual control). The dust collector begins offline pulse jet cleaning by stopping the airflow to individual compartments in sequence.
The PLC programmable control instrument follows the preset differential pressure control program. For each compartment:
The exhaust valve of one compartment is closed, stopping airflow through the filter bags in that compartment.
Pulse valves are then opened row by row, using low-pressure compressed air to perform pulse jet cleaning on the filter bags.
The dislodged dust collects in the hopper and is discharged by a rotary discharge valve into the ash conveying system below.
After cleaning is completed for that compartment, the exhaust valve is opened to restore filtration.
The cleaning cycle then proceeds to the next compartment.
Recommended Products
Search from here
Get Free Quotes